How to Measure Volumetric Flow and Set the Limit
If you push your printer faster than its hotend can melt filament, you get under-extrusion. Volumetric flow is the number that tells you where that wall is. This guide shows you how to find it and how to lock it in so Orca Slicer enforces it automatically.
What Volumetric Flow Actually Means
Volumetric flow rate is the volume of molten filament your hotend pushes through the nozzle per second, measured in cubic millimeters per second (mm³/s). It connects three print settings that are usually tuned separately: layer height, line width, and print speed.
Example: 0.2 mm layer × 0.44 mm width × 150 mm/s speed = 13.2 mm³/s
Your hotend has a physical ceiling—a maximum rate at which the heater block and melt zone can liquefy filament. Above that ceiling, the drive gear moves faster than the melt zone can keep up, causing filament slip and gappy layers. The limit in Orca Slicer tells the software where that ceiling is, so it can cap speed automatically.
The Quick Manual Estimate
Before running a test print, you can estimate whether your current settings are close to the limit. Open your current profile in Orca Slicer and find these three values:
- Layer height: e.g., 0.2 mm
- Line width: typically 0.4–0.5 mm
- Print speed: highest speed for perimeters/infill
If the result is already above 20–25 mm³/s on a standard 0.4 mm all-metal hotend, you are likely at or over the limit and may be getting under-extrusion without knowing it.
Use this as a safety check, but always run a physical test for accuracy.
How to Run the Step-Up Test
Find or generate a step tower
Create a tower in Orca Slicer using height-range modifiers. Start at 5 mm³/s and increase by 2–3 mm³/s per step up to 35 mm³/s.
Match speed to volumetric flow
Use Speed = Flow ÷ (Height × Width) to set the print speed for each segment of the tower.
Print and inspect
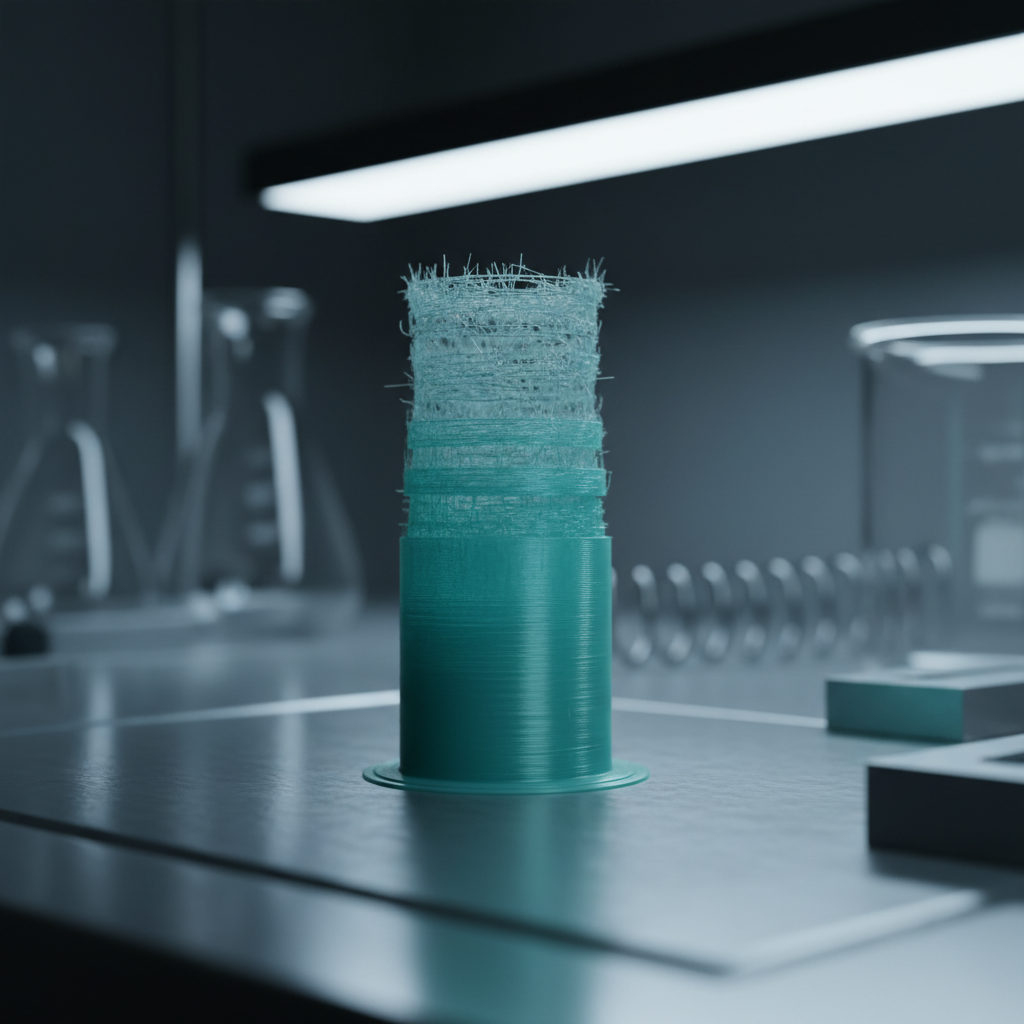
Inspect each step: surface should be smooth. Look for the transition where it first loses its shiny appearance or shows gaps.
Record the value
Note the flow rate of the last good step. Your physical limit sits just beyond that point.
Apply a Safety Margin
Running at the absolute limit leaves no room for error. Best practice is to reduce your measured limit by 10–20%.
"For example: if under-extrusion starts at 20 mm³/s, a 10% margin puts your safe limit at roughly 16-18 mm³/s."
Enter the Value in Orca Slicer
- Open Filament settings for your tested material.
- Go to the Advanced section of the Filament tab.
- Locate the Max volumetric speed field.
- Enter your safe limit (e.g.,
16) and save.
When the Limit Changes
Nozzle Diameter
Larger nozzles (0.6mm+) push significantly more material than standard 0.4mm units.
Material Type
PLA, PETG, and TPU all have different melt viscosities and flow characteristics.
Print Temperature
Increasing temp by 15°C raises the limit; cooler temps reduce it substantially.
Hotend Upgrades
High-flow hotends have much longer melt zones and higher ceilings than standard units.
How Orca Slicer Enforces the Limit
Once set, Orca Slicer uses this value as a hard ceiling. It checks every toolpath move. If the combination of layer height, line width, and requested speed exceeds the limit, the slicer silently reduces the speed to stay within the cap.
Automated Physics
You don't have to manually calculate safe speeds for every profile; the software handles it for you.
Quality Protection
If a print seems slower than expected, the volumetric cap is likely active and protecting your print quality.
Related Guides and Tools
Common Questions
What is a good max flow for a standard 0.4 mm brass hotend?
My tower looks fine at 30 mm³/s. Should I still add a margin?
Does the limit apply to travel moves?
Will this make all my prints slower?
Try It in Orca Slicer
Orca Slicer includes the Max volumetric speed field in every filament profile. Download it free, run the test, and let the slicer handle the physics.
No ads · Free · Open-source
Includes built-in calibration tests for all your filaments.